

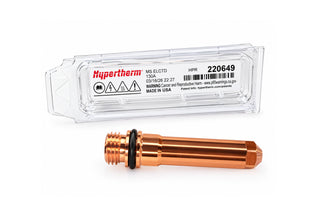
Genuine Hypertherm HyPerformance (HPR) electrode for 130 A bevel cutting of mild steel with a bevel-capable HPR torch, using oxygen as the plasma gas and air as the shield gas. It carries the cutting current and contains the hafnium insert from which the plasma arc is emitted, in a geometry suited to the extended bevel front end. Replace it when the insert reaches its wear limit, ideally together with the matching 130 A bevel nozzle.
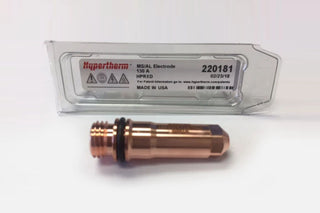
Genuine Hypertherm HyPerformance (HPR) electrode for 130 A mechanised plasma cutting of mild steel, using oxygen as the plasma gas and air as the shield gas. The electrode carries the cutting current and contains the hafnium insert from which the plasma arc is emitted. As the insert wears, arc starts and cut quality decline, so the electrode should be replaced when the pit depth reaches the limit in the Hypertherm manual. For best results replace it together with the matching 130 A nozzle.
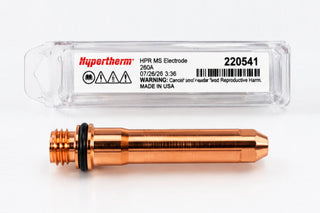
Genuine Hypertherm HyPerformance (HPR) electrode for 260 A bevel cutting of mild steel with a bevel-capable HPR torch, using oxygen as the plasma gas and air as the shield gas. Designed for the extended front-end geometry used when cutting at an angle to prepare weld edges, it carries the cutting current and contains the hafnium insert where the plasma arc is generated. Replace it when the insert reaches its wear limit, ideally together with the matching 260 A bevel nozzle.
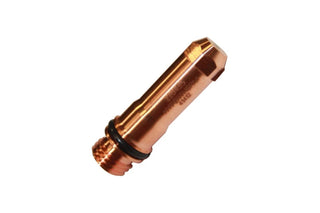
Genuine Hypertherm HyPerformance (HPR) electrode for 260 A mechanised plasma cutting of thick plate mild steel, using oxygen as the plasma gas and air as the shield gas. The electrode carries the high cutting current and contains the hafnium insert from which the plasma arc is emitted. Replace it when the insert is worn to the limit in the Hypertherm manual to maintain arc stability and protect the nozzle, ideally together with the matching 260 A nozzle.
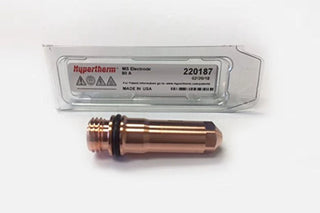
Genuine Hypertherm HyPerformance (HPR) electrode for 80 A mechanised plasma cutting of mild steel, using oxygen as the plasma gas and air as the shield gas, suited to thinner plate. The electrode carries the cutting current and contains the hafnium insert where the plasma arc is generated. Replace it when the insert is worn to the limit in the Hypertherm manual to maintain reliable arc starts and consistent cut quality, ideally together with the matching 80 A nozzle.
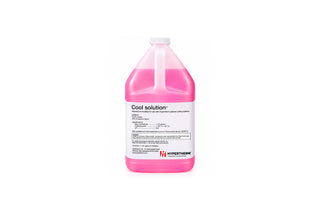
Genuine Hypertherm torch coolant for liquid-cooled Hypertherm plasma systems, supplied in a 1 US gallon (3.8 L) container. The pre-mixed coolant (de-ionised water with 30% propylene glycol) circulates through the torch to remove heat from the electrode and nozzle, which is critical for consumable life and consistent cut quality. It protects against freezing and has the low conductivity required in a plasma torch, so plain tap water or automotive antifreeze should not be used in its place. Replace the coolant at the intervals given in your system's operator manual.
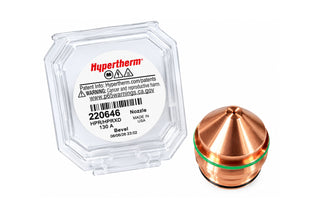
Genuine Hypertherm HyPerformance (HPR) nozzle for 130 A bevel cutting of mild steel with a bevel-capable HPR torch, using oxygen as the plasma gas and air as the shield gas. Designed to give clearance to the plate when the torch is tilted, it allows accurate bevelled weld-preparation edges to be cut. The precision orifice constricts and focuses the plasma arc; replace the nozzle when the orifice is worn, oval or damaged. Use with the matching 130 A bevel electrode and shield.
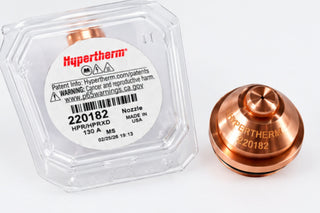
Genuine Hypertherm HyPerformance (HPR) nozzle for 130 A mechanised plasma cutting of mild steel, using oxygen as the plasma gas and air as the shield gas. The nozzle's precision orifice constricts and accelerates the plasma arc, producing the narrow, high-energy jet that delivers HPR cut quality. Replace it when the orifice becomes worn, oval or damaged, as this causes bevelled edges, wider kerf and increased dross. Use with the matching 130 A electrode, shield and swirl ring.
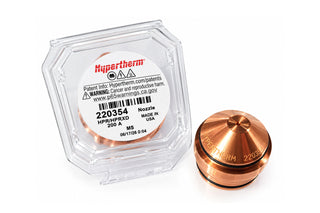
Genuine Hypertherm HyPerformance (HPR) nozzle for 200 A mechanised plasma cutting of medium to thick plate mild steel, using oxygen as the plasma gas and air as the shield gas. The nozzle constricts and focuses the plasma arc through a precision orifice, determining kerf width, edge squareness and dross levels. Replace it when the orifice is worn, out of round or damaged. Use with the matching 200 A electrode, shield and swirl ring.
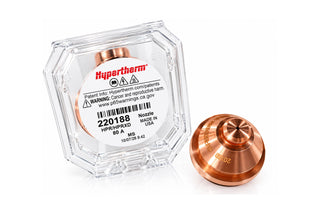
Genuine Hypertherm HyPerformance (HPR) nozzle for 80 A mechanised plasma cutting of mild steel, using oxygen as the plasma gas and air as the shield gas, suited to thinner plate. The nozzle's precision orifice constricts the plasma arc into a fine, focused jet for a narrow kerf and clean, square edges. Replace it when the orifice is worn or damaged. Use with the matching 80 A electrode and shield.
Genuine Hypertherm HyPerformance (HPR) nozzle assembly for 260 A bevel cutting of mild steel with a bevel-capable HPR torch, using oxygen as the plasma gas and air as the shield gas. Its geometry is designed to give clearance to the plate when the torch is tilted, so that accurate bevelled weld-preparation edges can be cut on thick plate. The precision orifice constricts and focuses the plasma arc; replace the nozzle when the orifice is worn or damaged.
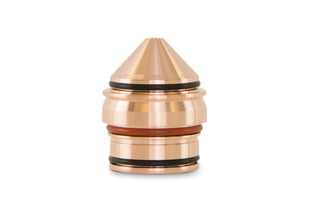
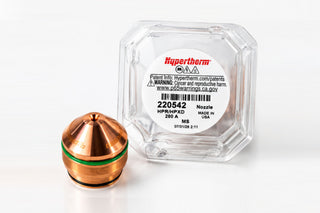
Genuine Hypertherm HyPerformance (HPR) nozzle assembly for 260 A mechanised plasma cutting of thick plate mild steel, using oxygen as the plasma gas and air as the shield gas. The nozzle constricts the high-current plasma arc through a precision orifice to deliver a narrow, high-energy cutting jet with square edges and low dross. Replace it when the orifice is worn or damaged. Use with the matching 260 A electrode and shield.
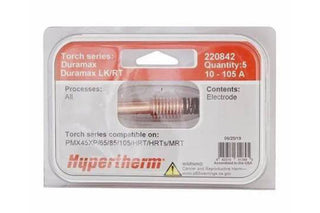
Genuine Hypertherm electrode for Powermax plasma systems, used across the 10 A to 105 A range. The electrode carries the cutting current and contains the hafnium insert from which the plasma arc is emitted. Replace it when the insert is pitted to the depth specified in the Powermax manual to maintain reliable arc starts and consistent cut quality, ideally together with the nozzle.
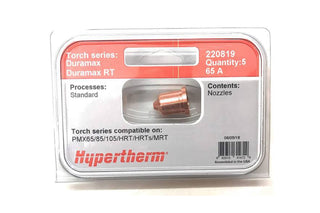
Genuine Hypertherm Duramax nozzle for Powermax plasma systems, for cutting at 45 A to 65 A with air or nitrogen. The nozzle constricts the plasma arc through a precision orifice to produce a focused, high-velocity cutting jet. Matching the nozzle to the cutting current gives the best cut quality and consumable life. Replace it when the orifice is worn or out of round.
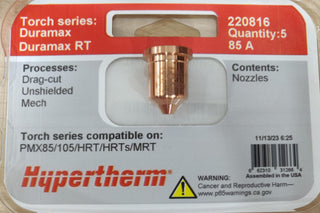
Genuine Hypertherm Duramax nozzle for Powermax plasma systems, for cutting at 65 A to 85 A with air or nitrogen. The nozzle constricts the plasma arc through a precision orifice to produce a focused, high-velocity cutting jet. Using the nozzle that matches your cutting current gives the best cut quality and consumable life. Replace it when the orifice is worn or out of round.
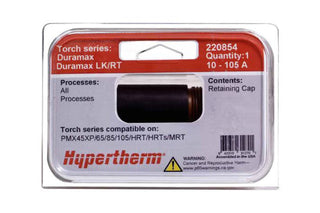
Genuine Hypertherm Duramax retaining cap for hand-held and mechanised Powermax plasma torches, used across the 10 A to 105 A range. The retaining cap screws onto the torch head and holds the nozzle and swirl ring firmly in their correct positions, ensuring proper alignment and gas flow. It is a longer-life part than the electrode and nozzle, but should be replaced if it is cracked, heat-damaged or no longer seats the consumables securely.
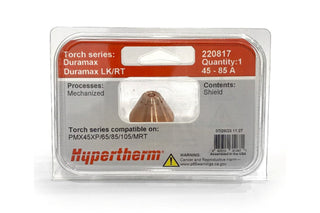
Genuine Hypertherm Duramax shield for mechanised (machine-mounted) Powermax torches, for cutting at 15 A to 85 A. The shield fits over the front of the torch, protecting the nozzle from molten metal during piercing and cutting and helping to direct the airflow around the arc for cleaner cuts. Replace it when damaged or heavily spattered to protect the nozzle and maintain cut quality.
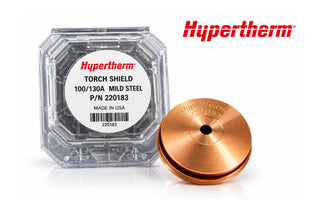
Genuine Hypertherm HyPerformance (HPR) shield for 130 A mechanised plasma cutting of mild steel, using oxygen as the plasma gas and air as the shield gas. The shield is the outermost front-end consumable: it directs the shield gas around the arc to improve cut quality and protects the nozzle from molten metal splashed back during piercing. Replace it when the orifice is damaged or covered in spatter to protect the nozzle and maintain edge quality.
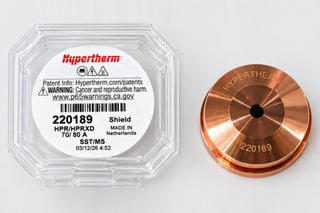
Genuine Hypertherm HyPerformance (HPR) shield for 70 A to 80 A mechanised plasma cutting of mild steel, using oxygen as the plasma gas and air as the shield gas. The shield directs the shield gas around the plasma arc for improved edge quality and protects the nozzle from molten metal during piercing and cutting. Replace it when the orifice is damaged or heavily spattered.
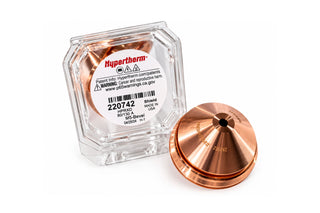
Genuine Hypertherm HyPerformance (HPR) shield for 80 A to 130 A bevel cutting of mild steel with a bevel-capable HPR torch, using oxygen as the plasma gas and air as the shield gas. Its tapered profile provides clearance to the plate when the torch is tilted, while directing shield gas around the arc and protecting the nozzle from molten metal. Replace it when the orifice is damaged or heavily spattered.